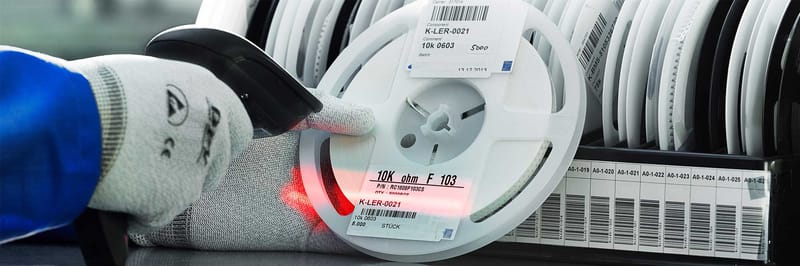
A traceability label is a machine-readable mark applied to a circuit board that uniquely identifies it. Scan it, and the manufacturing record for that individual assembly opens up: which work order it belongs to, which components went into it, which machine placed them, which operator ran the line, what the inspection systems saw, and how it performed at test.
As electronics manufacturing has moved towards tighter accountability and more automation, this has stopped being an optional extra. For regulated products it is a legal requirement. For everything else it is the difference between recalling one batch and recalling a year of production.
What a traceability label gives you
Scanning a single board recovers its production batch, the assembly line and machine logs, the operator, the inspection history, component lot and revision data, and the test results.
That record pays for itself in specific ways:
- Rapid defect isolation. When a failure appears in the field, the record tells you which boards share the suspect component lot or the suspect process window. You contain the batch instead of the year.
- Less scrap and rework. Faster diagnosis means fewer boards reworked speculatively.
- Process improvement. Aggregated traceability data exposes recurring failures and the stations that produce them.
- Automation. Barcodes are what let placement machines, inspection systems and repair stations attach their data to the right unit.
- Audits and compliance. A scan answers questions that would otherwise take a day of paperwork.
Where the code is actually read
The label is not read once. It is read repeatedly along the line, and every read attaches another record to the unit:
- MES scan-in at line load, registering the board
- Solder paste inspection (SPI) and automated optical inspection (AOI), attaching inspection results per unit
- Pick-and-place, associating placed-component lot data with the board
- X-ray (AXI), in-circuit test (ICT) and functional test (FCT)
- Conveyor handoffs between machines, and final pack-out
This is why placement accuracy and consistency matter so much. A label that a human can find is not the requirement; a label that a fixed camera can find, in the same place on every board of every repeat order, is.
Label materials and heat
Not every label survives soldering, and this is the most common practical mistake.
Polyimide labels rated to approximately 300 °C are the industry standard for application before soldering. That 300 °C figure is the label's rating and its safety margin -- it is not what the process demands. The actual thermal load is lower:
| Process | Typical peak temperature |
|---|---|
| Lead-free reflow | 245--260 °C |
| Wave solder pot | 250--265 °C |
| Vapour phase | ~230 °C |
Vapour phase is capped by the boiling point of the Galden fluid, which makes it the gentlest of the three, not the harshest. The rating gives comfortable headroom across all of them.
PET and polyester labels are rated roughly −40 to 150 °C with short spikes to around 200 °C. They do not survive reflow and must be applied after all soldering is complete.
The rule is simple: confirm the thermal rating in the label's product documentation. If a label is not approved for high-temperature exposure, it must be applied only after every soldering operation -- reflow, wave, vapour phase and rework -- has finished. If the assembly documentation does not say which, the line will guess.
Label sizes and the DataMatrix code
Our standard label sizes are 5 × 5, 7 × 7, 10 × 10 and 10 × 20 mm. Each carries a DataMatrix code containing the work order and the board's unique serial number, with optional human-readable text alongside it.
The code size is not a free choice, and it is worth showing the arithmetic because it determines whether the smallest label actually works.
DataMatrix ECC200 packs roughly two numeric digits per codeword, giving these numeric capacities: a 10 × 10 module symbol holds 6 digits, 12 × 12 holds 10, and 14 × 14 holds 16. An eleven-digit payload therefore does not fit a 12 × 12 symbol. The smallest usable symbol is 14 × 14 modules.
On a 5 × 5 mm label, a 14 × 14 symbol plus the mandatory one-module quiet zone on each side spans sixteen module widths. That works out to roughly 0.30 mm per module -- around 0.25 mm if the label keeps a print border. Factory machine vision reads that comfortably given adequate camera resolution; it is, however, below the conservative X-dimension minimums quoted for general-purpose barcode verification. If you are specifying a 5 × 5 mm label, specify the camera resolution with it, and grade the printed codes to ISO/IEC 15415 or ISO/IEC 29158 rather than assuming any scanner will read them.
Larger labels remove the constraint entirely. If the board has room, use it.
Serial number format
Our standard traceability format is eleven digits, YYWWWWWNNNN:
YY-- the yearWWWWW-- the work order number, five digitsNNNN-- the serial number within that work order, four digits
So 19012340001 is year 19, work order 01234, serial 0001.
One point of care: in component date codes across the whole industry, WW conventionally means the work week. Here the five digits after the year are the
work order, not a week number. If you are writing a parser against this format, or specifying it in a document that a supplier will read, say so explicitly. The
format also implies its own ceilings -- 99,999 work orders and 9,999 units per work order -- which are worth checking against your production volumes before
they bind.
Placing the label on the PCB
Because the code is read automatically by fixed cameras, the label must sit in the same place on every board of every repeat order. Consistency reduces read failures more than any other single factor.
- Have the fabricator print the label placement outline directly onto the board according to your specification, wherever possible. An outline removes the ambiguity entirely.
- Place the label on the SMD component side. If one side carries many SMD components and the other few, choose the side with more.
- Maintain at least 3 mm clearance from printed text and symbols, plated and non-plated holes, SMD pads, and the board edge.
- For wave-soldered assemblies, place the label on the component side to keep it out of the solder wave's thermal and chemical path. If the placement is unavoidably exposed, apply the label after wave soldering.
- Do not apply labels onto components unless it is explicitly requested.
- Apply the label to a flat surface, ideally over an area without copper beneath it.
That last rule deserves its reasoning, because the two cases are not the same and are often explained wrongly.
Over copper traces, the issue is topography. A 35 µm copper trace leaves a ridge under the solder mask. A label bridging trace edges makes incomplete adhesive contact, and after thermal cycling it lifts and peels. This is a real and common failure.
Over a copper plane, the issue is not adhesive heat damage -- the entire board reaches reflow peak regardless of what lies beneath any given point, and a solid plane is in fact the flattest and smoothest region of the board. The real concerns are thermal mass and stress: a large plane sinks heat during reflow and can starve nearby solder joints, and CTE mismatch at plane edges can drive solder-mask blistering. Avoiding large planes remains sound practice. Blaming the adhesive is not.
Other ways a board can be marked
Adhesive labels are the method we use, and they are not the only way a board can carry its identity. It is worth knowing what the alternatives are and why they do not replace a label.
Fab-etched DataMatrix codes are applied by the bare-board fabricator in copper or in the legend. They are durable and cost almost nothing, but they are fixed at fabrication time, so they can only carry a board or panel identifier -- never a work-order-specific unit serial assigned later.
Laser direct part marking burns the code into the solder mask or copper. It is permanent and survives wash and reflow, at the cost of the marking equipment and per-substrate calibration, and it too requires the serial to be known at the moment of marking.
Inkjet marking is cheap but offers lower contrast and durability, and can smear under flux and wash.
The deciding factor is when the serial number is assigned. Both alternatives above need it fixed before or during fabrication. Where the serial is allocated by the ERP system against a work order -- as it is in our process -- and has to be both human- and machine-readable, and replaceable if damaged, an adhesive label is the method that fits.
The standards
- IPC-1782 -- Standard for Manufacturing and Supply Chain Traceability of Electronic Products. It is risk-based rather than a simple class scheme, defining four levels of material traceability (M1 to M4) and four of process traceability (P1 to P4), where level 4 means a complete history of the unit and of every component in it.
- IPC-2591 (CFX) -- Connected Factory Exchange, the vertical machine-to-host messaging standard that carries this data to an MES.
- IPC-HERMES-9852 -- the digital replacement for SMEMA, passing board identity between machines along the line.
- ISO/IEC 15415 and ISO/IEC 29158 (AIM-DPM) -- print quality and direct-part-mark quality grading. Codes should be graded, not merely printed.
Regulated industries mandate traceability outright, and typically demand the upper IPC-1782 levels: automotive under IATF 16949, which requires serial-level tracking for safety-critical parts; medical devices under ISO 13485 and the FDA's UDI rules in 21 CFR Part 830, and under EU MDR 2017/745; and aerospace and defence under AS9100.
Custom labels
We can print custom traceability labels, including customer-specific labels through our customisation service. These are tailored to each assembly and are not limited to traceability -- customers request bespoke content, formats and identifiers to support their own production, organisational and labelling requirements.
To manufacture a customised label we need:
- A sample label image
- Label specifications, such as material and dimensions
- Label contents, such as part number and manufacturing date
- Any special instructions, including whether the label must be applied before or after soldering
Traceability is one of the least glamorous investments in electronics manufacturing and one of the highest-returning. If you would like to discuss label specification, placement, or the traceability level your product needs, our team is happy to help.
Sources
- IPC-1782 -- Standard for Manufacturing and Supply Chain Traceability of Electronic Products
- IPC-2591 -- Connected Factory Exchange (CFX)
- IPC-HERMES-9852 -- Global Standard for Machine-to-Machine Communication in SMT Assembly
- ISO/IEC 15415 and ISO/IEC 29158 -- barcode and direct-part-mark print quality
- ISO/IEC 16022 -- Data Matrix bar code symbology specification (ECC200)
- J-STD-020 -- Moisture/Reflow Sensitivity Classification for Nonhermetic Surface Mount Devices (reflow profiles)
- IATF 16949, ISO 13485, 21 CFR Part 830 (UDI), EU MDR 2017/745, AS9100